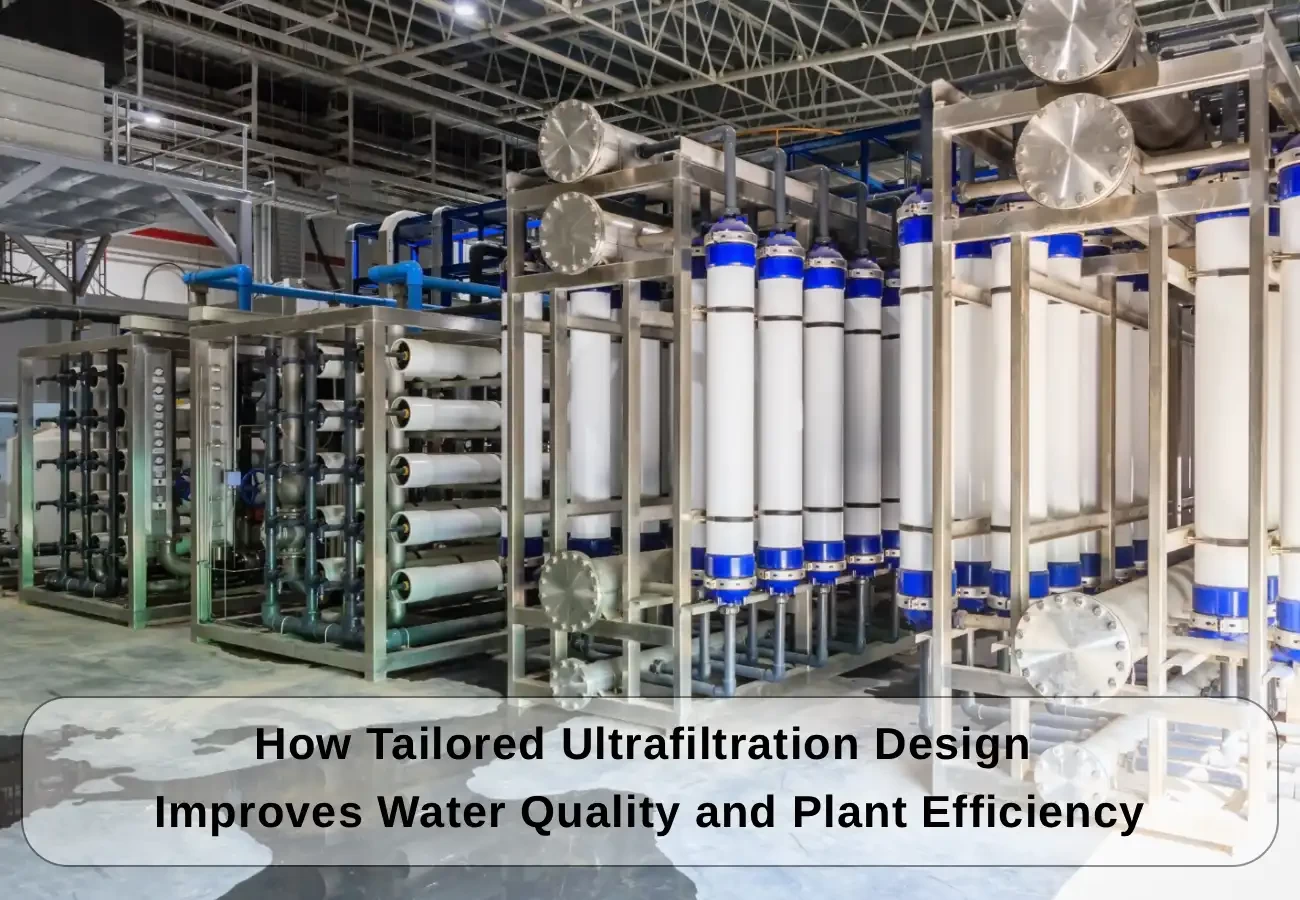
How Tailored Ultrafiltration Design Improves Water Quality and Plant Efficiency
Different industries have different water challenges. And the Ultrafiltration System should be different as well?
Ultrafiltration (UF) has become one of the most reliable technologies in the industry for the production of high-quality water. But here’s a question that many industries miss:
Can one ultrafiltration system work the same way in a food processing plant, a pharmaceutical facility, a tyre manufacturing unit and a bottled water plant?
The answer is No.
While membrane technology may look the same, the success of an ultrafiltration system is based on how well it is engineered for the specific application. A “one size fits all” design often leads to increased operation costs, unnecessary membrane fouling, frequent maintenance and inconsistent water quality.
At Alantech we do not believe that the right ultrafiltration system can be chosen from a catalogue- it is engineered around your process.
Every Industry Has a Different Challenge
Food & Beverage
Water quality directly influences the product quality and food safety.
The UF system must reliably remove suspended solids, bacteria and colloidal particles and must be able to operate with stable production and minimal downtime.
Bottled Water Plants
Consistency is important.
Water quality changes could impact consumer confidence and regulatory compliance. Well-designed UF systems provide reliable pretreatment for RO or final polishing application.
Also Read: ultrafiltration vs reverse osmosis
Pharmaceutical Industry
Even slight changes in water quality can affect the manufacturing process.
These facilities need highly reliable systems with hygienic design, validated performance and strict operational control.
Industrial Manufacturing
Factories often experience different quality of feed water throughout the year.
An ultrafiltration system shall be designed to withstand seasonal variations, turbidity fluctuations or fluctuations in contaminant loads.
This takes some careful engineering, not just bigger membranes.
The Alantech Approach
At Alantech we don’t start with equipment
We start with questions.
- What is your source water?
- What are your production objectives?
- How many hours a day will the system run?
- Is the water quality seasonal?
- What are your capabilities for maintenance?
- Are you looking to expand in the future?
We only recommend an ultrafiltration configuration once these answers are understood.
This first-of-its-kind engineering approach enables customers to realize stable performance, reduced operating costs and longer membrane life
Experience Builds Better Engineering
Alantech has been working with industries for years where water quality has a direct impact on both production efficiency and product quality.
One thing has remained consistent:
The most successful ultrafiltration systems are not the most expensive, but the ones specifically designed for the application.
We don’t sell the same system to every customer, we tailor the design to the operating environment, water characteristics and business objectives.
We have built long-term relationships with industries where reliability is valued over short-term cost savings, and that philosophy has helped us grow.
Also Read: Microfiltration and Ultrafiltration
Let's Design a System That Fits Your Industry
Each facility has unique water challenges, production goals and operational needs.
At Alantech, we design ultrafiltration systems from real process conditions, not generic templates.
Whether you are designing a new water treatment plant, upgrading an existing system or looking to improve operational performance, our team can help you find the right ultrafiltration solution for your application.
Because in ultrafiltration, one size does not fit all industries - and your business deserves a solution designed for you.