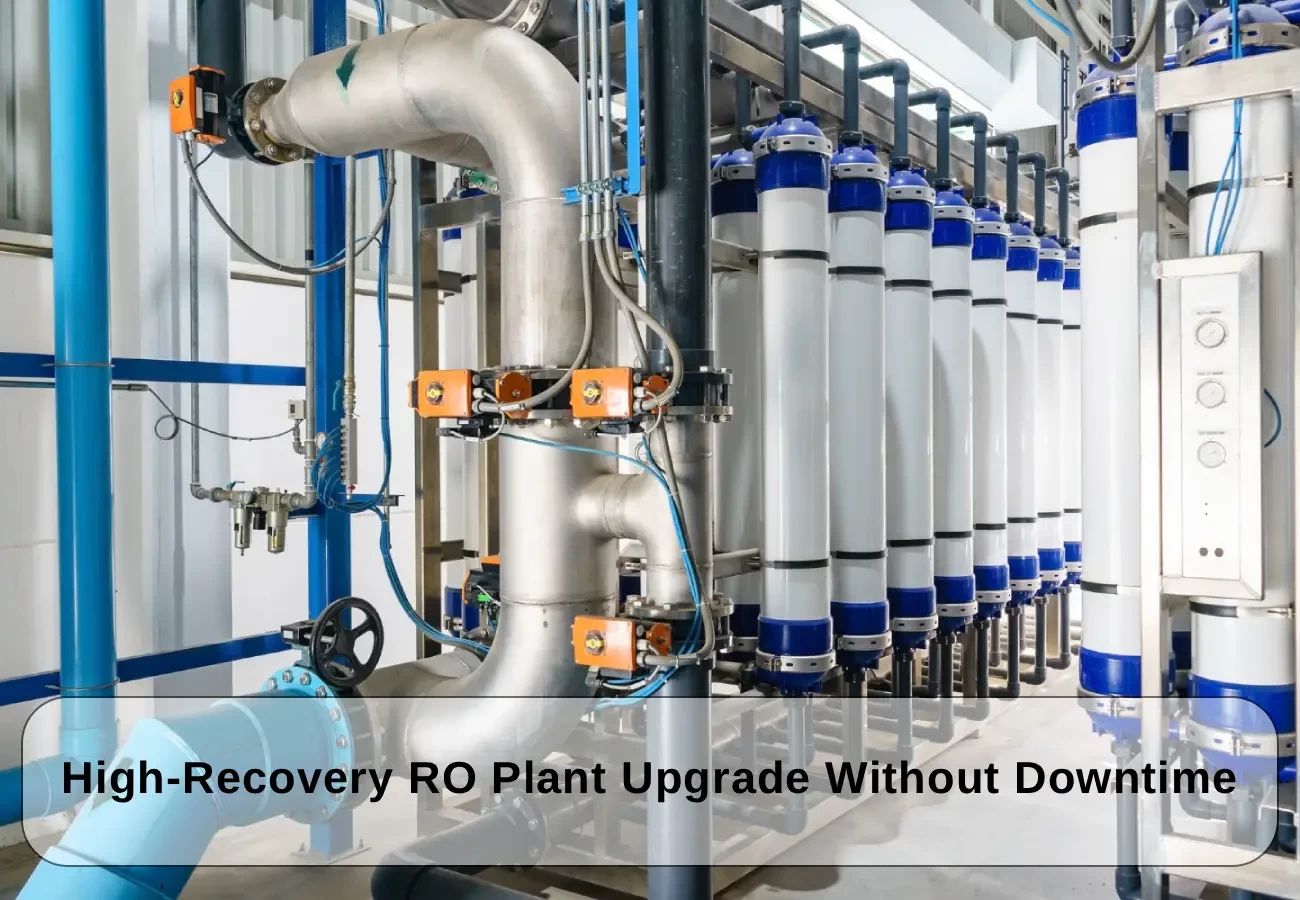
High-Recovery RO Plant Upgrade Without Downtime
A municipal water treatment upgrade combining 85% stated water recovery, ozone-system improvements and precision mineral dosing to achieve a 100 ppm TDS target.
Overview
When a major public water supply authority faced deteriorating output from an outdated ultrafiltration (UF) facility, it needed a complete plant overhaul. Alantech engineered a turnkey high-recovery RO plant rated at 15 m³/hr, replacing ultrafiltration with reverse osmosis (ultrafiltration to reverse osmosis) at 85% water recovery. Precision mineral dosing brings the permeate back to a 100 ppm TDS target, and the changeover was delivered with zero unplanned downtime.
Challenges in Upgrading an Existing Municipal Water Treatment Plant
The requirement was to replace the entire treatment system with an advanced reverse osmosis (RO) process and precision mineral dosing without causing a single minute of water supply disruption.
The project faced three main challenges:
- Operation without downtime: As one of the most important water providers in the region, the authority could not shut down operations. Decommissioning the existing UF plant and setting up the new RO plant had to be done quickly and within a very tight schedule.
- Deteriorating existing equipment: The existing ozone contact tank had experienced extensive thinning of its walls.
- TDS and taste: All dissolved solids had to be removed from the raw water, which was then remineralised back to 100 ppm TDS.xx
To understand why this conversion matters, read about the difference between ultrafiltration and reverse osmosis.
Alantech Solution
Replacing Ultrafiltration with a 15 m³/hr High-Recovery RO Plant
Alantech provided a custom-designed industrial water purification skid, built for maximum efficiency and quick setup. At its core is a 15 m³/hr high-rejection RO plant whose membranes deliver 85% water recovery, leading to minimal wastage of water.
Maintaining Continuous Water Supply Through Phased Commissioning
The design included a temporary bypass system and a quick modular setup, so the existing ultrafiltration system could be demobilised without disturbing production rates. This phased commissioning approach kept the continuous water supply running while the new RO plant was brought online.
Ozone Contact System Upgrade and Precision Mineral Dosing
The old ozone tank was replaced with a modernised oxidation system to manage microbial activity effectively.
Alantech also added a precision chemical injection skid for remineralisation of the zero-TDS permeate. Through precise dosing of calcium chloride, potassium bicarbonate and magnesium sulphate, the precision mineral dosing system maintains a 100 ppm TDS mineral water profile.
Results: 85% Water Recovery and a 100 ppm TDS Target
| Metric | Achieved Parameter |
| Plant Capacity | 15 m³/hr |
| System Recovery Rate | 85% (high-efficiency permeate yield) |
| Final Product Quality | 100 ppm TDS target mineral balance |
| Production Impact | 0 hours of unplanned downtime during installation |
| Operational Performance | Exceeded all design parameters post-commissioning |
Scale Your Water Infrastructure with Alantech
From highly sophisticated municipal installations to state-of-the-art commercial bottling plants, Alantech offers turnkey membrane-based solutions in the most demanding operating conditions. Explore our full range of water treatment systems.
Partner with Alantech for reliable, high-recovery, low-maintenance water purification.
Contact Alantech for a High-Recovery RO Plant Solution